SHELTERALL – RICHEL GROUP

SHELTERALL – RICHEL GROUP

#shelter #storage #bulk storage #storage shelter #big bag storage #asphalt aggregates

ABOUT US :

SHELTERALL® – Modular Storage Solutions for Environmental and Recycling Sites

Turnkey, foundation-free, and fully modular, SHELTERALL® shelters are designed for waste management, recycling platforms, depollution, and composting sites. They protect materials from bad weather, dust, and contamination, ensuring safe, compliant, and efficient storage.

Key Benefits:

  • Weather Protection & Quality Preservation: Keeps waste and recycled materials dry, clean, and safe. Reduces odor, spills, and contamination.
  • Modular & Flexible: Easily dismantled, extended, moved, or joined to create new storage cells. Wide range: 8–25 m width, up to 15 m ridge height.
  • Safe & Compliant: Meets ICPE regulations, water treatment requirements, and Building Eurocodes. Flame-retardant tarpaulins and TOUTABLOC® concrete blocks ensure fire safety and site security.
  • Optimized Access & Storage: Designed for easy loading/unloading, batching, and stock rotation. Openings, ventilation corridors, and nets improve handling and site hygiene.
  • Cost-Effective & Eco-Friendly: Reduces earthworks, adapts to any surface (earth, asphalt, slabs), and supports sustainable operations.

Applications:

  • Bulk waste storage
  • Sorting platforms and recycling cells
  • Depollution and hazardous material containment (asbestos, contaminated soils)
  • Composting operations with odor management

Why Choose SHELTERALL®?
Reliable, durable, and adaptable, our metal-textile buildings help environmental professionals optimize site operations, protect materials, and meet ecological and regulatory requirements. Quick to install and fully turnkey, SHELTERALL® is the solution for modern, safe, and efficient environmental storage.
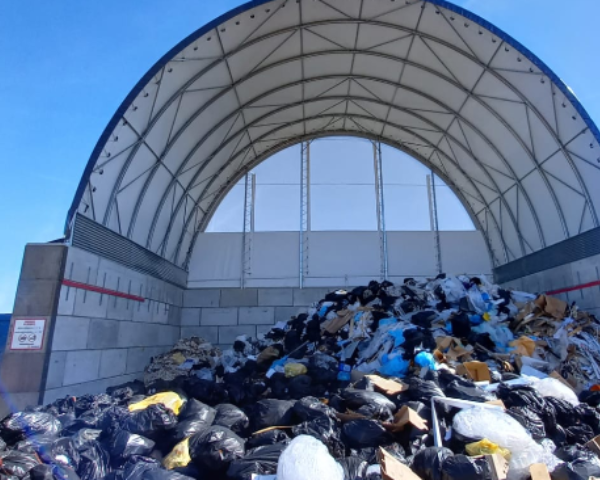
SHELTERALL® Bulk Storage is the turnkey, foundation-free solution for recycling professionals. Ideal for paper, cardboard, plastic, glass, metal, wood, eco-furniture, and construction waste, it provides high working volumes with extra-wide models (up to 25 m) and a free-standing arch for easy unloading with heavy machinery. Modular and scalable, it allows batch separation, side or gable access, and open-air storage areas. Compliant with Building Eurocodes and environmental regulations, flame-retardant sheets and fire-resistant TOUTABLOC® concrete blocks ensure safe, durable, and flexible bulk waste storage.
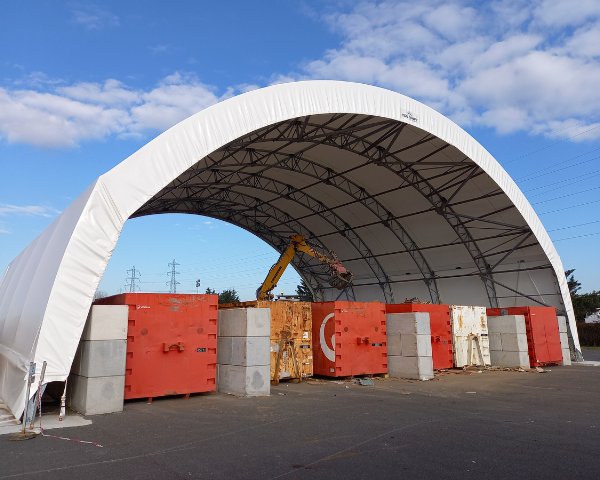
SHELTERALL® Sorting Areas – the ultimate modular, foundation-free solution for recycling and waste management. Designed with optimized height, volume, and safety options, it’s perfect for environmental companies and manufacturers managing waste recovery. Flexible, cost-effective, and fully modular, SHELTERALL® makes recycling, reuse, and waste treatment simple and efficient. Sturdy sorting cells comply with Building Eurocodes, ensuring a safe, durable, and professional workspace that adapts to your growing needs.
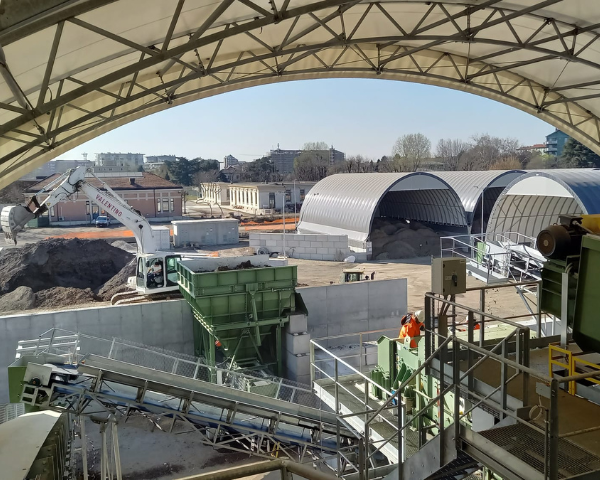
SHELTERALL® Depollution offers flexible, secure, and modular shelters for depollution, dismantling, and hazardous waste management. Recommended by environmental companies and vehicle scrapyards, it protects materials, soil, and groundwater while enabling recycling and safe storage. Foundation-free and adaptable to any surface, shelters can be quickly deployed, moved, or dismantled. Modular cells allow batching of contaminated materials, and TOUTABLOC® blocks ensure strength and safety. Insulated, soundproofed, and naturally lit, SHELTERALL® provides a safe, efficient, and comfortable workspace.
OUR ECO-RESPONSIBLE COMMITMENTS

The SHELTERALL® is made in France. It benefits from the technology and reliability of the Richel Group (the leading European producer of shelters). Its galvanised steel structure is compliant with the NF EN 13031-1 European standards and the Eurocodes building requirements. Its coated canvas covering is guaranteed for 10 years (see General Terms and Conditions of Sale). Our products are designed in accordance with Eurocode Building requirements by our design office and checked by partner inspection organisations.

NEW INNOVATION

Discover our photovoltaic-compatible storage solutions at our stand!

L'accès à ce contenu peut entraîner le dépôt de cookies par le fournisseur de la plateforme concernée. Si vous souhaitez continuer et afficher le contenu, vous devez nous donner votre consentement en cliquant sur le bouton ci-dessous.

CONTACT US

Sylvain DEGENS
Sales manager


Quartier de la Gare – 13810 – Eygalières – FRANCE

www.shelterall.eu

LEVIATHAN DYNAMICS

LEVIATHAN DYNAMICS

#evapoconcentration #effluent #reuse #wastewater #decarbonation #lowtemperature

ABOUT US :

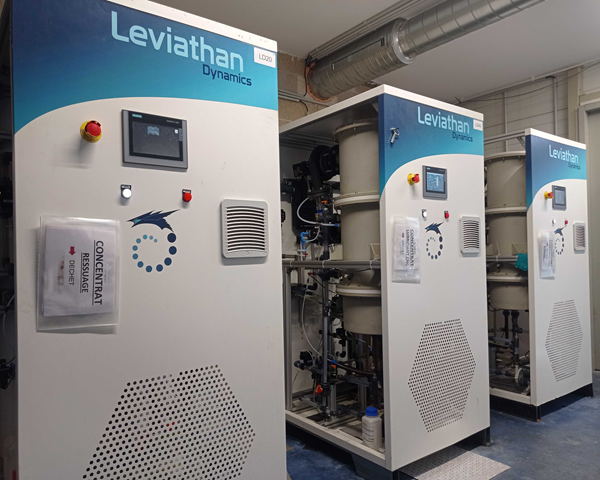
Leviathan Dynamics designs high-efficiency machines for water recycling and for cooling, reducing energy consumption by 30%.

Leviathan Dynamics started with a single idea in mind: replacing hazardous and polluting refrigerants by water. Since 2016, we’ve been struggling with the main technological barrier: the unavailability of compact and affordable compressors that work under vacuum.

We developed a unique technology that makes possible the use of mechanical vapor compression under deep vacuum. This technology is a combination of:

  • A patented high speed compressor design that makes possible the use of MVC without having to use expensive and massive compressors
  • A deep understanding of wet vacuum environment that allows us to design affordable vacuum management system
  • Internally developed numerical modelisation of evaporation and condensation required for efficient heat exchangers design

Leviathan Dynamics develops and markets a low-temperature evapo-concentrators that enables:

  • A reduction of at least 80% in the volume of industrial effluents to be treated, significantly lowering treatment costs and associated CO₂ emissions
  • Recovery and reuse of the water contained in effluents for reintegration into industrial processes
  • Solvent regeneration and concentration of valuable compounds
OUR ECO-RESPONSIBLE COMMITMENTS
  • Coq Vert
  • Team For The Planet
  • Solar Impulse Fondation
  • Gold Medal at the Geneva International Inventions Fair

NEW INNOVATION

Our low-temperature evapo-concentrator enables efficient wastewater treatment using an innovative vacuum mechanical vapor compression process, delivering very low energy consumption and a compact, easy-to-integrate design.

CONTACT US

Thomas BOULLY
Business Developper

E-mail : tboully@leviathan-dynamics.com
Tél. : +33 (0)7 49 98 64 23

1 Centre commercial de la tour – 93120 – La Courneuve – FRANCE

https://leviathan-dynamics.com/fr

LAB

LAB

#fluegastreatment #fluegascondensation #heatrecovery #biomass #wastetoenergy #carboncapture

ABOUT US :

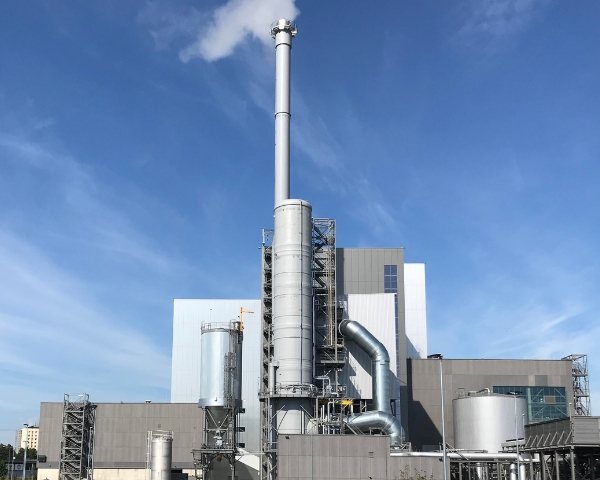
LAB is an engineering company specialized in the design, delivery, and upgrading of turnkey Flue Gas Cleaning Systems.
LAB is active worldwide on several applications: Energy from Waste (Waste-to-Energy), Sewage Sludge, Biomass as well as Diesel & Gas Engines for stationary and maritime power stations.

In recent years, LAB has expanded its technology portfolio by introducing Carbon Capture and Liquefaction Solutions, enabling customer plants to evolve towards a cleaner and more sustainable future.
With over 150 highly skilled specialists based in France (Lyon) and Germany (Stuttgart and Coburg), LAB has implemented more than 500 Flue Gas Treatment lines worldwide.

LAB is a subsidiary of MARTIN GmbH, a company specialized in the design, manufacturing, and construction of combustion systems and boilers for Waste-to-Energy plants, headquartered in Munich, Germany.

FLUE GAS TREATMENT

Specialist in industrial emission control, LAB designs and implements tailor-made solutions to manage air pollutants from Waste-to-Energy plants, biomass facilities, and mono-incinerators for sewage sludge. 

With a modular approach based on the Best Available Techniques (BAT), our solutions enable the control of the main pollutants: dust, acid gases, nitrogen oxides, heavy metals, dioxins, and furans, while ensuring advanced heat recovery through flue gas condensation.

In compliance with European (IED directive, BREF, etc.) and global regulations, our systems are designed and implemented to meet the specific requirements and challenges of each application.

HEAT RECOVERY

Heat recovery through flue gas condensation is becoming a crucial component in addition of traditional flue gas cleaning systems, significantly boosting overall plant efficiency and representing a high-impact opportunity. This technology by capturing residual heat from flue gases transforms lost energy into a valuable resource transferred to district heating networks.

High-performance flue gas condensation units offered by LAB can be easily integrated into both existing and new flue gas treatment processes. The system works by condensing the water vapor present in the flue gases and transferring the recovered heat to district heating network with support of heat pumps if needed. This recovered energy is thus valorized, contributing to the decarbonization of energy production.

CARBON CAPTURE

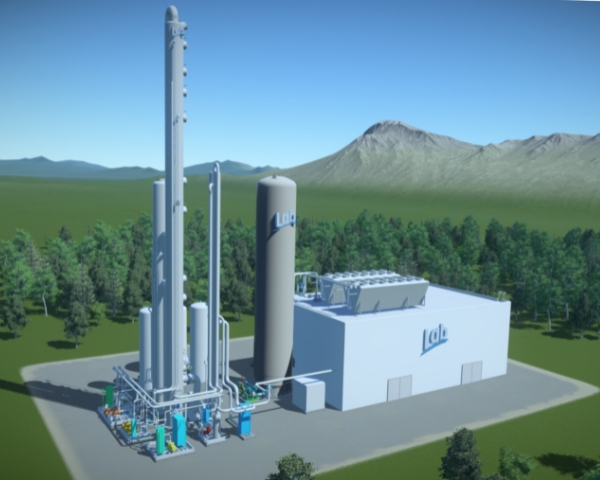
In a context where industrial decarbonization is a key challenge, LAB, as a specialist in flue gas emissions treatment and heat recovery, supports stakeholders in the Waste (WtE), Biomass (BtE) and Sludge (SSI) to Energy sector by offering reliable and tailored amine based Carbon Capture solutions for the reduction of their Carbon Dioxide (CO₂) emission.

Thanks to its expertise and proven technologies, LAB offers an integrated approach to capture the CO₂, allowing the interconnection with the flue gas treatment systems and the other parts of the facility.

In addition to the Carbon Capture System, LAB also includes CO₂ purification and conditioning steps, in partnership with leading companies in this field. The goal is to meet the high-quality standards required by the off-takers and end-users.

OUR ECO-RESPONSIBLE COMMITMENTS

We are certified ISO 14001, ISO 9001, ISO 45001

NEW INNOVATION

Development of Carbon Capture Solutions for Waste-to-Energy.

L'accès à ce contenu peut entraîner le dépôt de cookies par le fournisseur de la plateforme concernée. Si vous souhaitez continuer et afficher le contenu, vous devez nous donner votre consentement en cliquant sur le bouton ci-dessous.

CONTACT US

David BOYER
Sales Director

E-mail : david.boyer@lab.fr
Tél. : +33 (0)6 13 58 27 50

259 avenue Jean Jaures – 69007 – Lyon – FRANCE

lab.fr

INFIGROUP

INFIGROUP

#incineration #furnace #wastetoenergy #biomass #waste #wastemanagement

ABOUT US :

INFIGROUP, headquartered in Marseille, France, is a specialist in the design and manufacture of waste incineration systems, delivering tailor-made solutions for industrial and environmental applications. As a major international player in combustion-based waste treatment, INFIGROUP has built its reputation on robust and proven technologies recognized for their efficiency, reliability, flexibility, and ease of operation.

Present on four continents, INFIGROUP generates nearly 90% of its revenue internationally through a strong global network of around fifty qualified distributors. The company supports its clients throughout the entire project lifecycle, from engineering and manufacturing to installation, commissioning, and on-site training delivered by its experienced technical teams.

INFIGROUP offers a comprehensive range of biomass boilers designed to convert waste into sustainable energy. These solutions enable the recovery of a wide variety of biomass resources, including forestry residues, non-usable wood, urban green waste, and agricultural by-products such as rice straw, olive pomace, palm oil EFB, coconut shells, and sugarcane bagasse. INFIGROUP is a trusted supplier for biomass power plants and energy recovery projects worldwide.

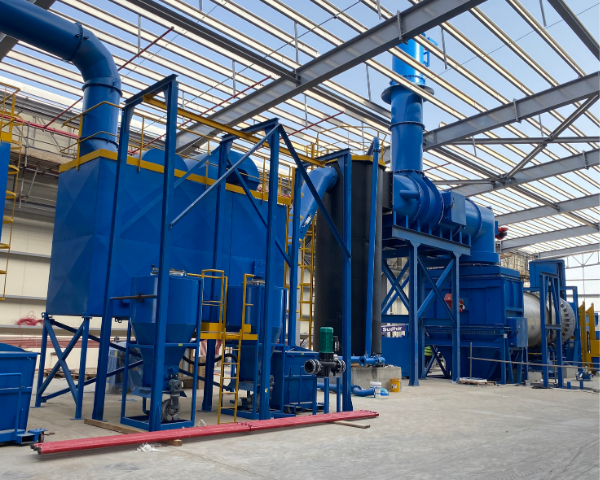
In the field of incineration, INFIGROUP provides equipment for the treatment of all types of solid and liquid waste, from compact units to complete incineration lines. Its technologies, based on static furnaces and rotary kilns, cover capacities ranging from 5 kg/h to 5 000 kg/h. INFIGROUP also integrates advanced flue gas treatment systems and heat recovery solutions, enabling steam production, cooling, or electricity generation through Waste-to-Power processes.

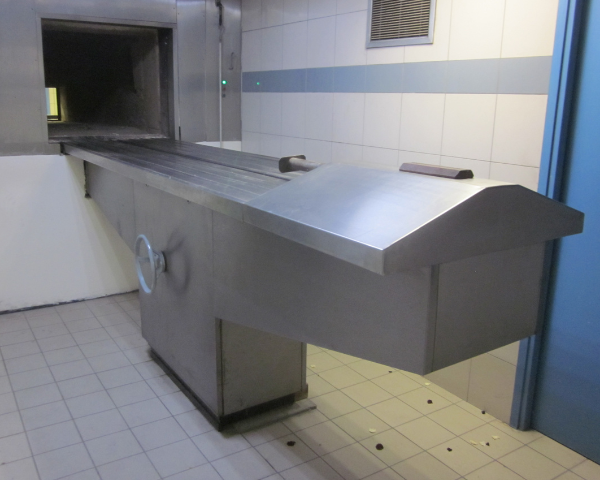
INFIGROUP also designs and manufactures turnkey cremation systems, installed in buildings or containerized units. These robust and high-performance solutions ensure efficient, automated cremation cycles while meeting strict environmental standards.

Since 1999, INFIGROUP has been developing solutions for biomass energy production and for the treatment of healthcare, industrial, animal, and petroleum waste. The company also supplies flue gas filtration systems and loading equipment, now essential for regulatory compliance and emissions control.

With references worldwide, INFIGROUP is a reliable partner for projects ranging from simple biomass installations to complex incineration plants and energy recovery facilities, combining technical expertise with a strong commitment to sustainable and innovative solutions.

Incinerators

INFIGROUP offers a full range of equipment designed to treat all types of solid and liquid waste, from compact incinerators to complete incineration lines. A wide selection of technologies based on static furnaces and rotary kilns covers capacities from 5 kg/h to 5,000 kg/h per treatment line. The LCI range (static furnace) handles 5–100 kg/h, the HDI range (static furnace) 100–3,000 kg/h, and the FRI range (rotary kiln) 500–5,000 kg/h. INFIGROUP also provides tailored flue gas treatment and heat recovery solutions, enabling the production of steam, cooling, or electricity through Waste-to-Power systems, for all types of waste.

Cremation

INFIGROUP designs, manufactures, and markets turnkey cremation systems, installed in buildings or containerized units. These innovative and robust systems ensure a minimum of six cremations per eight-hour shift, with cremation cycles ranging from 40 to 70 minutes and requiring no operator intervention. For all products, installation, on-site commissioning, and operator training are provided by INFIGROUP teams. Since 1999, INFIGROUP has specialized in waste incineration solutions, biomass-based heat production, and the treatment of healthcare (DASRI), industrial, animal, and petroleum waste. INFIGROUP also supplies flue gas filtration systems and loading skips, essential for emissions control and regulatory compliance.

Biomass Boilers

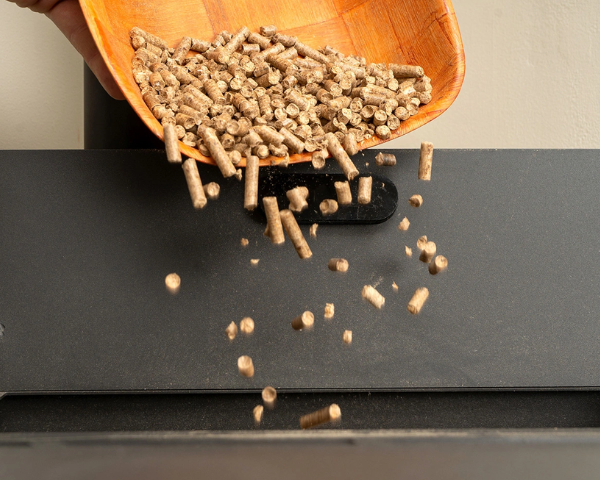
INFIGROUP offers a complete range of biomass boilers designed to convert waste into energy. These systems process forestry residues and non-usable wood, urban green waste (pruning, grass clippings), and agricultural by-products such as rice straw, olive pomace, palm oil EFB, coconut shells.

NEW INNOVATION

We work to transform the waste into suistanable energy such as hot water for sanitary use, coolers and electricity.

CONTACT US

Patrice FAVEROT
CEO

E-mail : p.faverot@infigroup.fr
Tél. : +33 (0)7 86 52 99 65

565, Avenue du Prado – 13008 – Marseille – FRANCE

www.infigroup.fr

KINEIS

KINEIS

#IoT #connectivity #satellite #satelliteiot #IoTConnectivity #SatCom

ABOUT US :

Kinéis: Satellite IoT for Remote Water Monitoring
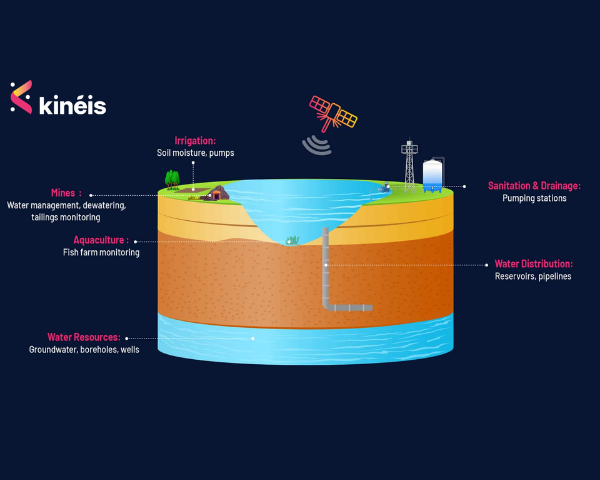
How do you monitor buried pipelines, mountain reservoirs, or isolated pumping stations when there is no cellular network and no power supply?

Kinéis operates a dedicated constellation of 25 satellites, designed specifically for low-power IoT, enabling reliable and cost-efficient connectivity anywhere on Earth at scale
It is particularly relevant in areas where terrestrial networks are unavailable or not economically viable

Data is automatically collected and transmitted within minutes, with no on-site intervention

Kinéis integrates seamlessly into existing environments. We do not replace your infrastructure.

Depending on your needs, Kinéis connectivity can be deployed:

  • through ready-to-use solutions and turnkey integrations for rapid deployment
  • or through our certified partner ecosystem (VAM program), where manufacturers integrate our KIM2 module directly into their devices

In all cases, compatibility with standard industrial sensors (4-20mA, Modbus, SDI-12) and seamless integration with existing SCADA and data platforms are ensured

Devices operate autonomously for years using long-life batteries, with no external power required. This makes Kinéis particularly relevant for off-grid and hard-to-access water infrastructure.

What Kinéis changes for water operators:

  • From manual inspections to continuous remote monitoring
  • From data gaps to reliable, structured time-series
  • From delayed reactions to early anomaly detection

Key applications:

  • Remote infrastructure monitoring (pipelines, pumping stations, reservoirs)
  • Groundwater and surface water level monitoring
  • Water quality and environmental data collection

With Kinéis, previously unreachable assets become fully visible. Operators reduce field operations, improve responsiveness, and gain actionable data to optimize performance

Extend your monitoring to every critical asset, anywhere.

Meet us at IFAT Munich 2026 to explore concrete deployment use cases and partnerships

CONTACT US

Angelo RANDRIA
Business Line Manager

E-mail : arandria@kineis.com
Tél. : +33 (0)6 72 44 91 99

11, rue Hermès – 31520 – Ramonville-Saint-Agne – FRANCE

www.kineis.com

EMO

EMO

#sludgetreatment #wastewater #septage #sewage #effluent

ABOUT US :

EMO is a leading engineering company in the design, manufacturing, installation of electromechanical equipment and turnkey solutions for sewage, septage, wastewater and drinking water plants including:

– pre-treatment (fine and coarse screens, screw conveyors,  classifiers), – sludge treatment (gravity belt thickeners, belt filter press, plate filter press, peripheral equipment), – dryers, – equipment for contaminated grit (grit from waste water treatment plants, from sewerage systems, street sweepings, oil grit, etc) into following solids such as wash drums, grabs,  – equipment for the treatment of industrial effluent : sludge from surface treatment, food industries, chemical industries, mineral industries, – design and installation of compact wastewater treatment plant as well as septage treatment plant, – turnkey installations, – sludge analysis (tests in laboratory), – commissioning of equipment and after-sales service.

EMO now has equipment installed in more than 120 countries, sold through an established network of more than 70 agents or distributors around the world!

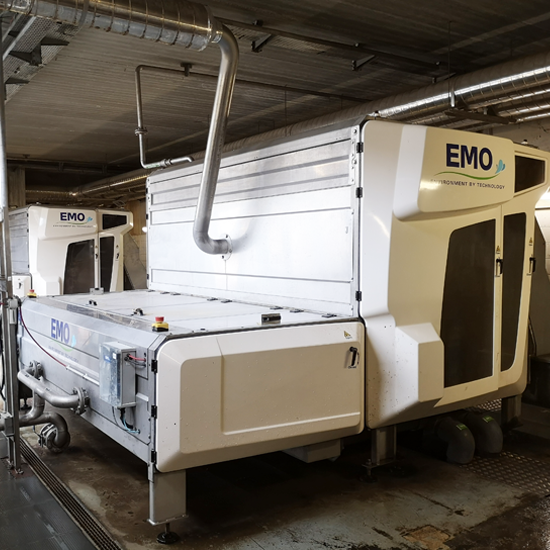
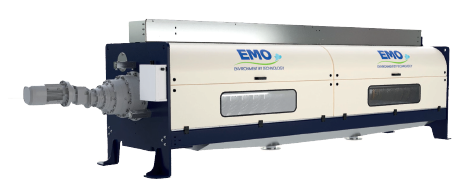
Belt filter press OMEGA NHP – sludge dewatering @EMO

The Belt filter press OMEGA NHP has been developped by EMO for continuous dewatering of municipal and industrial sludge.

The sludge is processed in three distinct stages: flocculation, gravity drainage and pressing.

Advantages:

  • Long term reliability thanks to an increased frame structure made of galvanized and stainless steel profiles
  • Optimum space requirement/efficiency ratio
  • No civil works constraint (machine equipped with adjustable feet)
  • New roller configuration for optimised sludge treatment
  • Belt length specially designed for a greater progressive sludge pressing for maximum dryness
  • Easy maintenance and supervision.

OMEGA SSP Screw press

EMO strong of its long history of designing and manufacturing dewatering technology, has developed its own range of sludge screw presses: more efficient and maintenance friendly machines.

All sludge screw presses OMEGA SSP conception has been given to equipment life time, performance, low operational cost and easiest parts replacement.

Sludge screw presses OMEGA SSP as per all other dewatering technology is design to dewater any industrial or municipal thickened sludge.

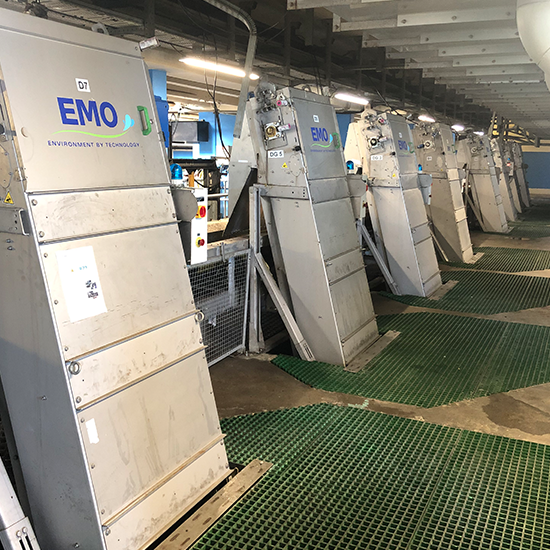
AQUARAKE – inclined multirake bar screen

The AQUARAKE is an inclined continuous bar screen with fixed bar rack and multiple rakes driven by chains.

This kind of screen can be used for many applications: pumping and filtering stations (irrigation, flood control, rain sewerage network), municipal treatment plant, drinking water plants, water intakes (cooling water for hydro power plants and refineries), industrial water processes and wastewater treatment plants.

The AQUARAKE bar screen can be used as a coarse screen as well as a fine screen: bar spacing from From 50 mm down to 6 mm.

Two ranges available:

  • DIXM with a reinforced HDPE guide system
  • DIM with stainless steel gears and high resistance bearings.
OUR ECO-RESPONSIBLE COMMITMENTS

ECOVADIS – SILVER // ISO 9011 ISO 14001

Motivated by a desire to act responsibly and sustainably, EMO has integrated a voluntary Corporate Social Responsibility approach at the heart of its short, medium and long-term global strategy.

Our approach is fully in line with the guidelines of the Global Compact (to 2030) and the 26000 standard, which aims to reconcile three key factors: environmental commitment, social balance and economic development. Our CSR policy goes hand in hand with our commitment to excellence, innovation and integrity for our stakeholders. Here’s one of our commitments:

NEW INNOVATION

OMEGA SSP SCREW PRESS

https://www.youtube.com/channel/UCwQmY3UAGYxP533h7C5hKRg

CONTACT US

Olivier CHAGOT
Export Sales Manager

E-mail : chagot@emo-france.com
Tél. : +33 (0)6 09 96 96 79 – +33 (0)2 99 86 15 22

Parc d’activités de la Richardière, 4 rue l’Epine – BP 53209 – 35532 – Noyal-sur-Vilaine Cedex – FRANCE

https://www.emo-france.com/

GRAVIFLOW

GRAVIFLOW

#flowmeter #gravityflow #accuaraty #water #sewage #innovation

ABOUT US :

Graviflow is a French startup that manufactures water flowmeters with an innovative patented technology.

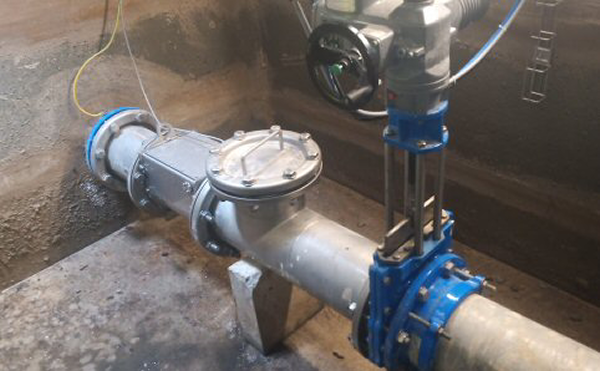
Our water flowmeters are very precise, better than 98% exactitude, from small flows, on an effective range of 0.1% to 100% of the nominal flow, very easily to install on existing hydraulic structures without requiring significant work and are “plug & play”.

Our flowmeters are made of robust 316L stainless steel, machined with great precision.

Our flowmeters are made in standard diameters from DN100 to DN1200.

The maintenance is reduced. GRAVIFLOW flowmeters can be controlled on site without disassembly by a metrological procedure validated by water agencies.

We provide standard shims and gauges for in place metrological testing by the operator or an approved testing agency.

Available functions:

  • alarms on thresholds,
  • sampling equipment control,
  • flow regulation (valve control),
  • data logger option,
  • low power option.

Areas of use (typical):

  • sewerage networks,
  • water springs,
  • industrial fluid networks,
  • sewage treatment plants,
  • combined sewer overflows,
  • pumping stations inflow and overflow.

Decisive benefits:

  • Insensitivity to flow regime, even changing flow regimes,
  • Compact design,
  • No field adjustment required,
  • COFRAC connected hydraulic bench calibration certificate provided,
  • Low cost of the measuring point.

Hydraulic storage works
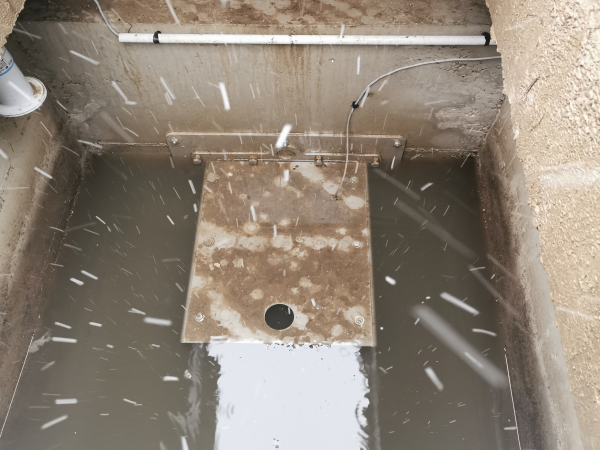
Overflow self-control on storm spillway

Characteristics of the work and installation

  • Passage manhole with entrance/exit
  • Discharge pipe: DN500
  • Nominal flow: 2100 m3/h
  • Downstream surface mounting on the upstream wall of the structure
  • Electronic box and display in the existing electrical cabinet

Operating conditions

  • Partially submerged and permanent pipe.
  • GRAVIFLOW model in V2 version adapted to flow measurement in conditions of downstream influence.
  • Taking into account the downstream level by radar probe.

Sending information to the existing Sofrel remote transmitter:

  • Continuous flow measurement: 4-20mA
  • Volume counting pulses: NO contact
  • Flow threshold over-threshold alarm: NO contact
  • Flow meter blocking alarm: NO contact

GRAVIFLOW, the solution in the case of gravity flow

The GRAVIFLOW process allows our flow meters to perform a fair and reliable measurement in most cases of gravity flow, and particularly in cases where other devices on the market are not satisfactory.

Best solution

When flow regimes are variable or turbulent our flow meter is the best solution.

Available functions

  • Real-time instantaneous flow measurement (4-20mA output)
  • Calculation of total volume
  • Volume counting pulses, not programmable
  • Alarm on high or low flow threshold
  • Measurement fault: blockage or internal fault
  • Intuitive local communication interface via Bluetooth

Pumping stations
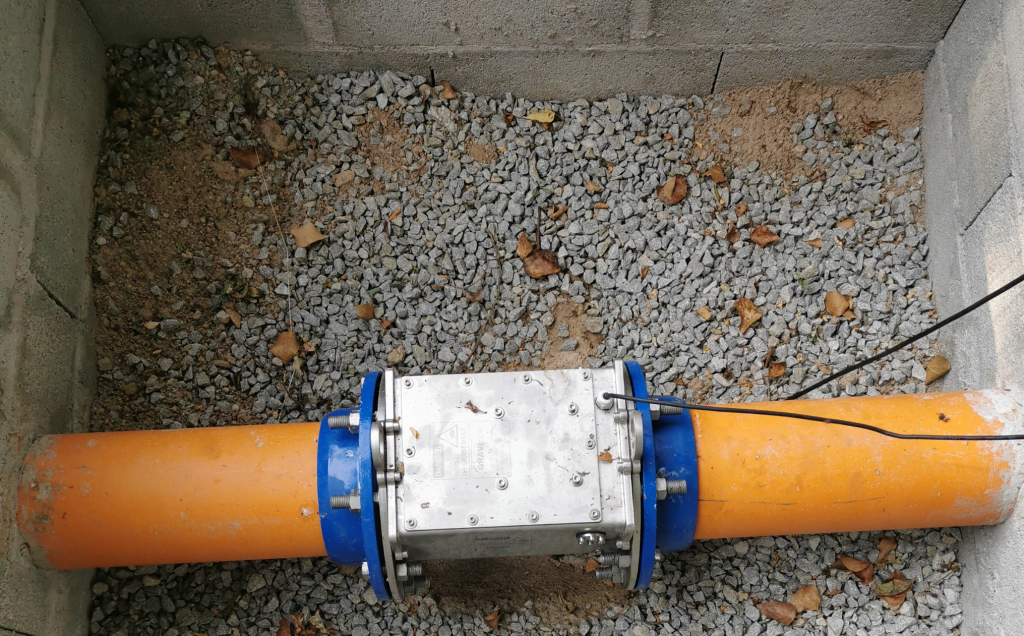
Pumping station overflow

Characteristics of the work and installation

  • Outlet sight too full pumping station
  • Discharge pipe: DN200
  • Nominal flow: 160 m3/h
  • Mounting between standardized flanges
  • Electronic box in electrical box nearby

Operating conditions

  • Partially filled/full pipe
  • GRAVIFLOW CLAP200 model in standard version

Sending information to the SOFREL remote transmitter of the SP:

  • Continuous flow measurement: 4-20mA
  • Volume counting pulses: NO contact
  • Flow threshold over-threshold alarm: NO contact
  • Flow meter blocking alarm: NO contact

Wastewater treatment plants
Flow regulation

Characteristics of the work and installation

  • Passage manhole with entrance/exit
  • Discharge pipe: DN200
  • Nominal flow: 160 m3/h
  • Mounting between flanges downstream of the control valve
  • Electronic box and display in the existing electrical cabinet

Operating conditions

  • Pipe partially filled.
  • GRAVIFLOW model in V1 version without downstream influence.

Sending information to the existing Sofrel remote transmitter:

  • Continuous flow measurement: 4-20mA
  • Valve control by existing automation
  • Volume counting pulses: NO contact
  • Flow threshold over-threshold alarm: NO contact
  • Flow meter blocking alarm: NO contact

L'accès à ce contenu peut entraîner le dépôt de cookies par le fournisseur de la plateforme concernée. Si vous souhaitez continuer et afficher le contenu, vous devez nous donner votre consentement en cliquant sur le bouton ci-dessous.

CONTACT US

Christian MARREIRO
CEO

E-mail : contact@graviflow.com
Tél. : +33 (0)7 77 77 66 33 – +33 (0)3 89 39 13 64

2 rue des Peupliers – 68920 – Wettolsheim – FRANCE

https://www/graviflow.com

GOMMAZONE

GOMMAZONE

#conveyor #rubberbelt #conveyorbelt #gommazone #pvcbelt #pubelt

ABOUT US :
Gommazone is a company specialized in the import and distribution of complete conveyor belt solutions. It offers a wide range of rubber, PVC and polyurethane conveyor belts suitable for industrial sectors such as food processing, logistics, quarries, recycling and material handling.

Through a network of carefully selected manufacturing partners known for their reliability and product quality, Gommazone provides products compliant with European standards while maintaining strong price competitiveness. The company acts as a direct link between manufacturing plants and conveyor maintenance and installation professionals (belt technicians, industrial maintenance companies, integrators and technical distributors).

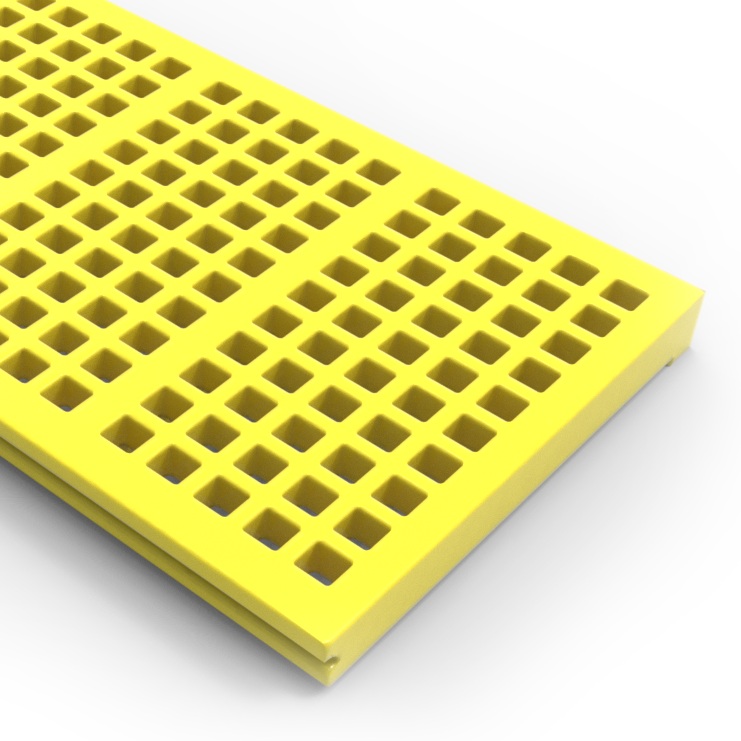
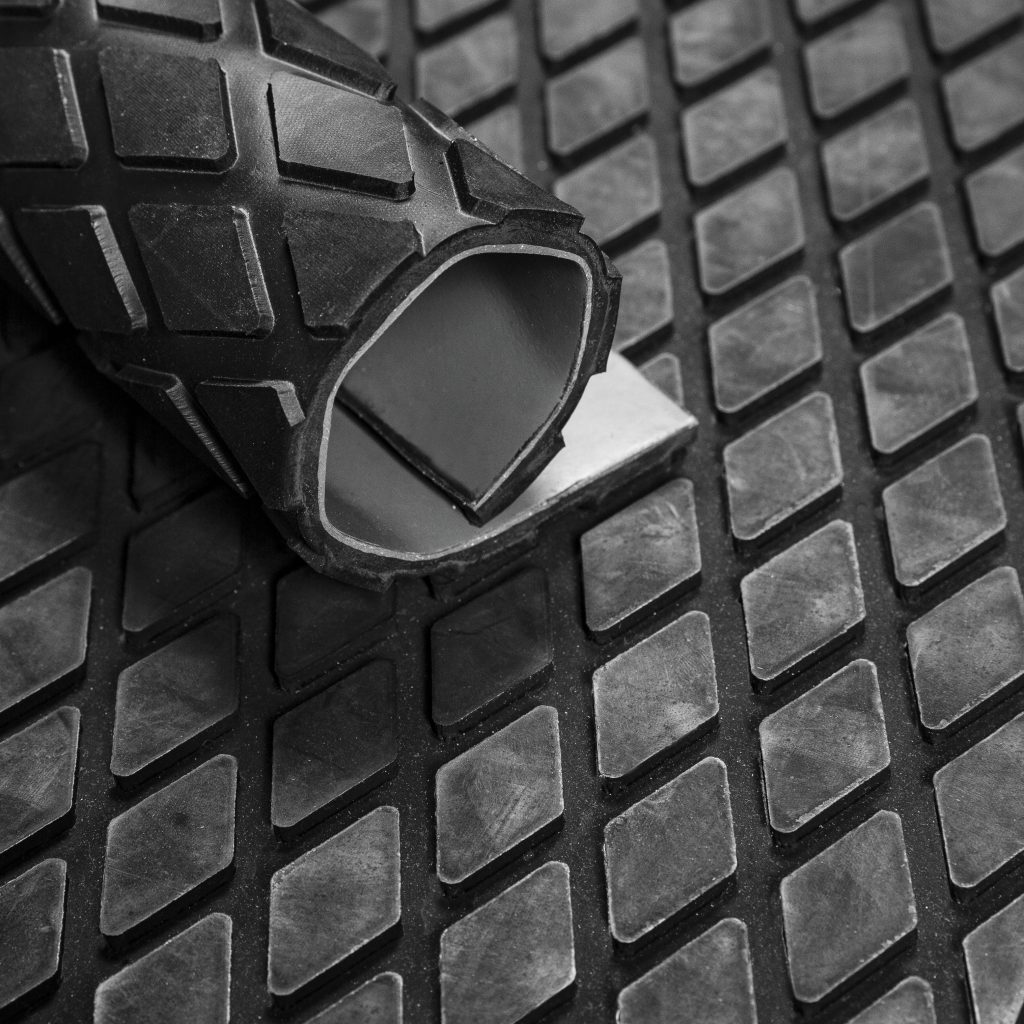
In addition to conveyor belts, Gommazone supplies all essential conveyor accessories including mechanical fasteners, pulley lagging, pulleys, curtains, guiding, screening media in polyurethane…

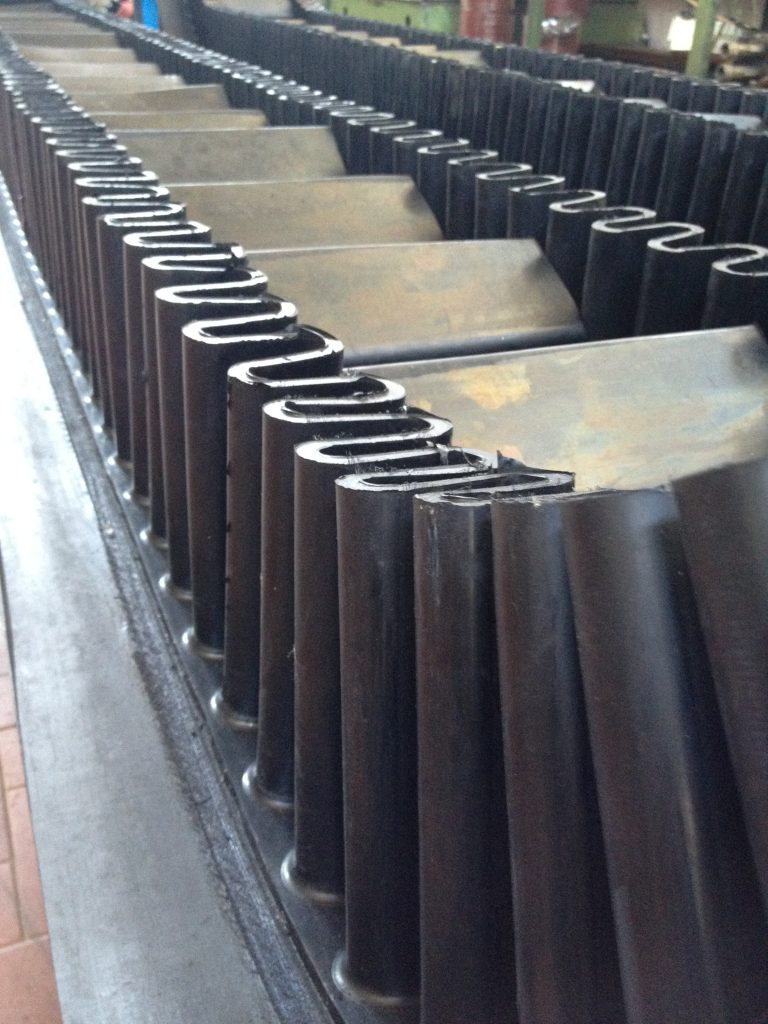
Gommazone stands out for its responsiveness, flexibility and technical support. The company can provide both standard products with short lead times and customized solutions designed to meet specific constraints such as heat resistance, abrasion resistance, food grade compliance, oil resistance, heavy loads or inclined conveying.

Gommazone’s objective is to become a long-term technical partner for its customers by ensuring product availability, expert advice and optimization of operating costs

Gommazone supplies : Rubber Belts : flat belts, chevron belts, custom-made belts, PVC and Polyuréthane belts

Gommazone also supplies screening media

Gommazone supplies a wide range of conveyor accessories as pulley lagging, rubber and polyurethane sheet, lateral curtains…

CONTACT US

Guillaume COUPEZ
CEO

E-mail : gcoupez@gommazone.fr
Tél. : +33 (0)6 88 67 79 25

Usine des Dunes, Rue des Acièries – 59495 – Leffrinckoucke – FRANCE

www.gommazone.fr

OMEAX

OMEAX

#Valve #actuator #control # Smart valve #IOT valve #Pressure management

ABOUT US :
OMEAX-Smart Flow Control for a Sustainable Future

Water is vital to life. Managing its pressure, flow, and quality is essential for sustainability and energy efficiency.

Omeax delivers complete valve solutions for water, building services, and industrial applications worldwide.

With more than 10 years of expertise in the valve industry, we support our partners with reliable, high-performance solutions tailored to demanding environments.


🌍 Water

Complete solutions for the entire water cycle:

  • Pumping stations
  • Distribution networks
  • Drinking water
  • Wastewater
  • Seawater applications

🏢 Building

Comprehensive solutions for:

  • Water supply
  • Fire protection
  • HVAC systems
  • Data centers

Fully compatible with BMS systems to improve energy efficiency and support green buildings.

🏭 Industry

Reliable solutions for:

  • High pressure & extreme temperatures
  • Steam & compressed air
  • Oil & gas
  • Chemical & corrosive fluids
  • Marine, sugar & ethanol, pulp & paper

Our Product Portfolio

Shut-off Valves
Butterfly, gate, globe, ball, and knife gate valves with electric, pneumatic, or hydraulic actuators.

Control Valves
Automatic control valve (ACV), pilot operated control valve, Pressure reducing valve, Plunger valve (Needle valve), motorised control valve.

HVAC Control
Modulating valves (two- or three-way) enable precise management of hot water, chilled water and air, in coordination with your building management system (BMS).
Double regulating valves, Differential pressure control valve

System Protection
Check valves, safety valves, air valves, and strainers for network reliability.

Wastewater Solutions
Knife gate valves, ball check valves, PVC valves and fittings

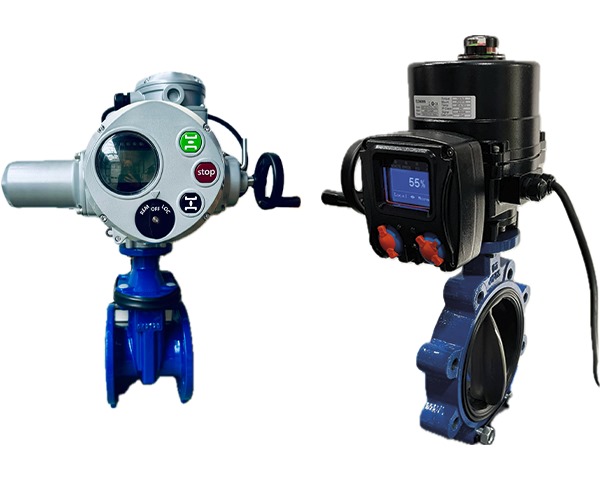
We are specialist of motorized valve. We provide automation solutions according to customer’s request:

 Electric actuator:

  • ¼ turn actuator: butterfly valve, ball valve
  • Multiturn actuator: gate valve, knife gate valve,
  • Liner actuator: globe valve

Pneumatic actuator:

  • Double acting pneumatic actuator
  • Single acting pneumatic actuator

We deliver next-generation IoT Smart Control Valves and intelligent Pressure Management Solutions designed to transform water networks into efficient, data-driven systems.

💧 Reduce water losses
⚡ Cut energy consumption
📡 Monitor and control remotely in real time
📊 Turn operational data into actionable insights

Our smart technologies optimize performance, enhance reliability, and support sustainable infrastructure for utilities and industry.

Smarter pressure. Lower costs. Greater sustainability.

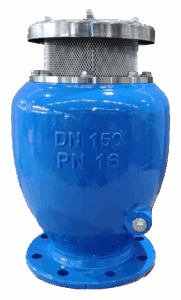
Air valves to protect network

NEW INNOVATION

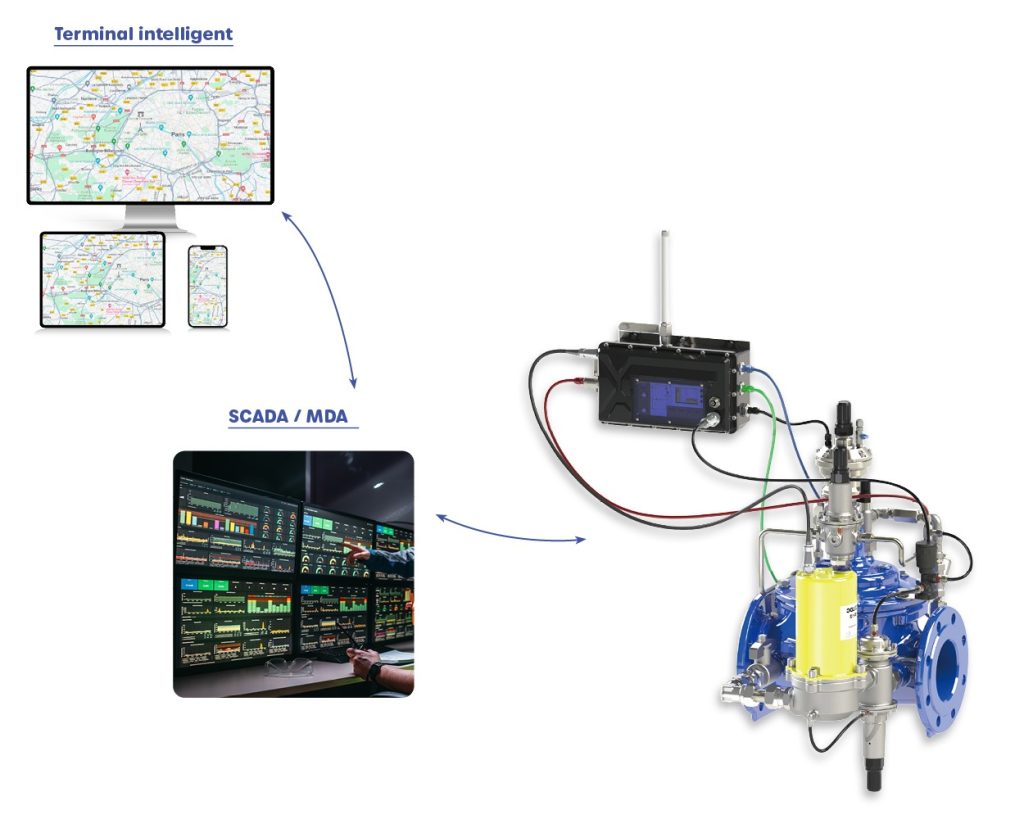
IOT  Smart valve : a valve equipped with sensors, an actuator, and communication technology that allows it to be monitored and controlled remotely via the Internet of Things (IoT).

It is used to automatically regulate the flow of liquids while sending real-time data to a SCADA system.

CONTACT US


Min JI
CEO

E-mail : jimin@omeax.com
Tél. : +33 (0)6 63 51 71 13 – +33 (0)3 85 97 09 81

19 rue Alphonse Lamartine – 71530 – Crissey – FRANCE

www.omeax.com

GL BIOCONTROL

GL BIOCONTROL

#Microbiology #DrinkingWaterQuality #WaterSafetyPlans #ATP-Metry #RapidTest #BacteriaLoadScreening

ABOUT US :

GL Biocontrol develops innovative microbiological monitoring kits that help water utilities, laboratories, and industrial operators ensure safe and high-quality drinking water. With over ten years of experience in rapid microbiological diagnostics, we design next-generation ATP-metry tests that support fast, reliable decisions directly in the field or in the lab.

Our core solution is a highly sensitive ATP rapid test specifically optimized for drinking water. By filtering a large 50 ml sample, the method provides the sensitivity needed for low-biomass waters and offers an immediate, clear view of microbial activity across treatment plants, storage zones, and distribution networks.

More than 600 public municipalities across Europe, as well as major private water operators, use our ATP-metry technology for routine monitoring and rapid troubleshooting. Its fast adoption demonstrates its reliability and operational value for day-to-day water-quality management.

Results are delivered in just a few minutes, enabling teams to act quickly without waiting for culture-based methods. This supports faster diagnostics, more responsive operations, and earlier detection of changes in the network.

Our rapid tests are supported by a dedicated mobile application that guides operators step-by-step, secures data, and generates standardized reports. The app also includes features for Water Safety Plans (WSPs), helping users document hazards, monitor control measures, and track microbiological trends with consistent traceability.

By combining high-sensitivity ATP detection, practical field workflows, and intuitive digital tools, our solution provides a modern alternative to traditional microbiological methods. We will be pleased to offer on-site demonstrations during the event, allowing visitors to discover the technology firsthand and experience how it can support operational control, compliance, and the delivery of safe drinking water.

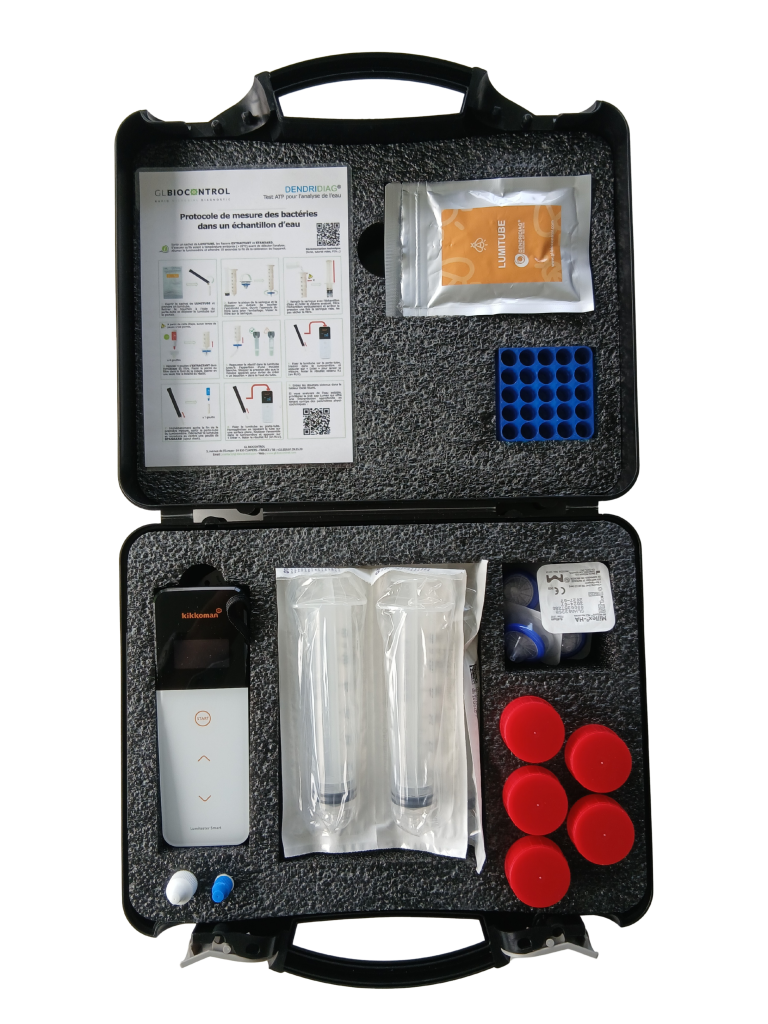
The complete ATP test kit comes in a compact field case containing a luminometer, filters, syringes, water sampling containers, a tube holder and reagent. All essentials are included to perform a full test in less than 3 minutes directly in the field or in the laboratory.

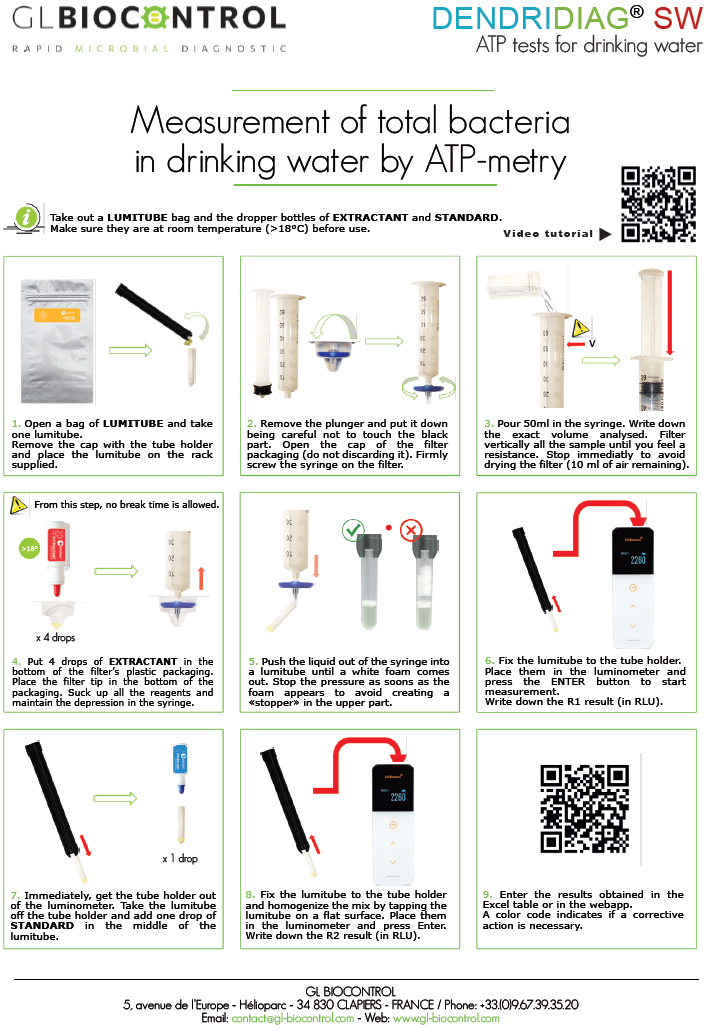
Our test protocol is designed for simplicity and can be performed directly in the field, even by operators without laboratory experience. The workflow starts with collecting a 50 ml water sample in a syringe. The sample is then filtered to capture the microorganisms on the filter. A reagent is added to release the ATP, and the resulting extract is transferred into our Lumitube for measurement with the luminometer. A standard is included to verify the reaction and ensure accurate quantification. All reagents can be stored for one year in the refrigerator or for three months at room temperature.

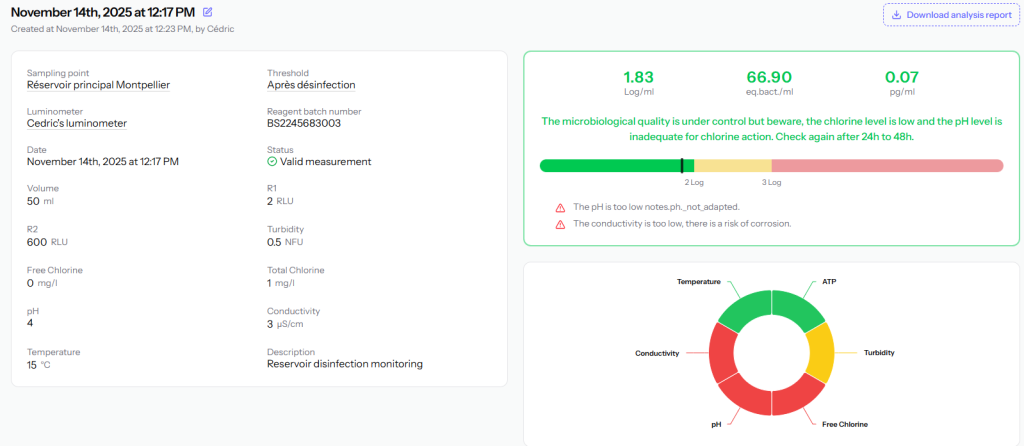
Our ATP kit includes a mobile app that makes reporting ATP test results easy, whether in the field or in the laboratory. It also provides automated result interpretation and records key drinking-water parameters such as chlorine, temperature, turbidity, etc. Over time, it offers a clear view of trends and control points, making it an ideal tool to support drinking-water network quality monitoring within “Water Safety Plans”.

NEW INNOVATION

Our kit and mobile app provide a modern way to monitor drinking-water quality, from the catchment area all the way to the tap. This innovation was first introduced in France and is now available across the rest of Europe.

L'accès à ce contenu peut entraîner le dépôt de cookies par le fournisseur de la plateforme concernée. Si vous souhaitez continuer et afficher le contenu, vous devez nous donner votre consentement en cliquant sur le bouton ci-dessous.

L'accès à ce contenu peut entraîner le dépôt de cookies par le fournisseur de la plateforme concernée. Si vous souhaitez continuer et afficher le contenu, vous devez nous donner votre consentement en cliquant sur le bouton ci-dessous.

CONTACT US


Cedric DEBONTE
Head of international sales

E-mail : c.debonte@gl-biocontrol.com
Tél. : +33 (0)6 08 49 93 55

5 avenue de l’Europe – Hélioparc – 34 830 – Clapiers – FRANCE

www.gl-biocontrol.com